———— Solvent Refining Solution for Base Oil
Base Oil Solvent Extraction Engineering Solution
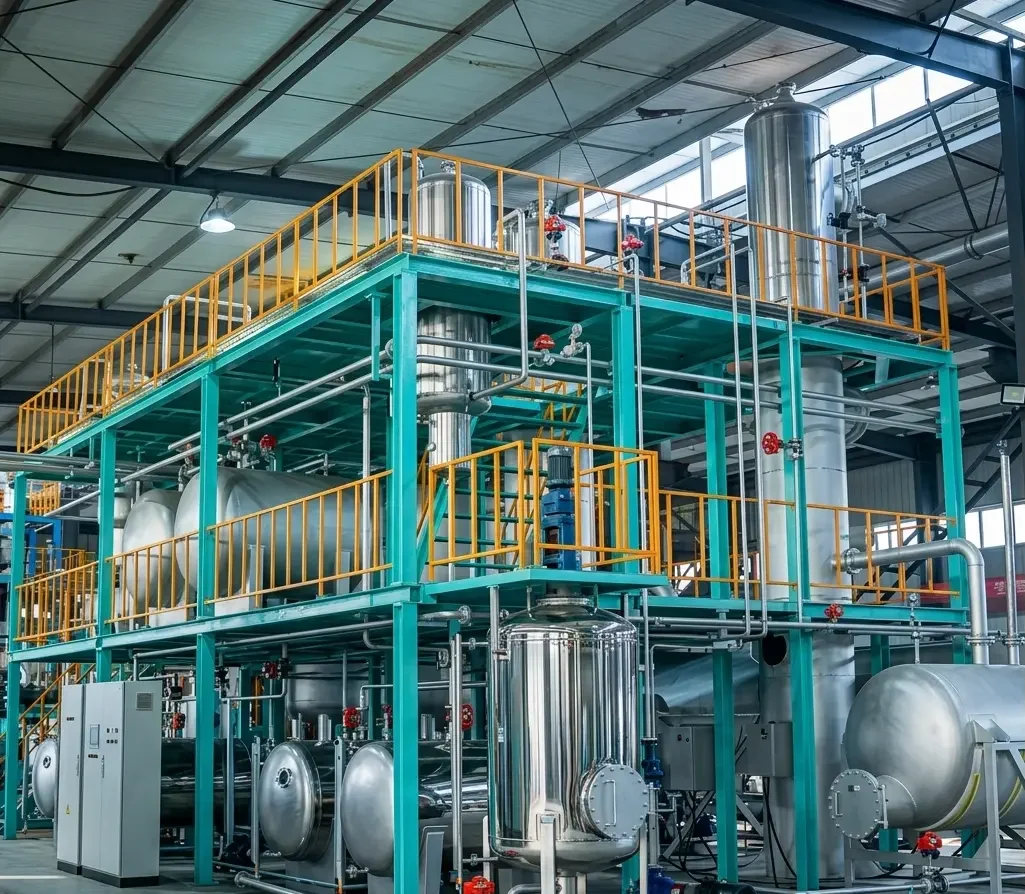
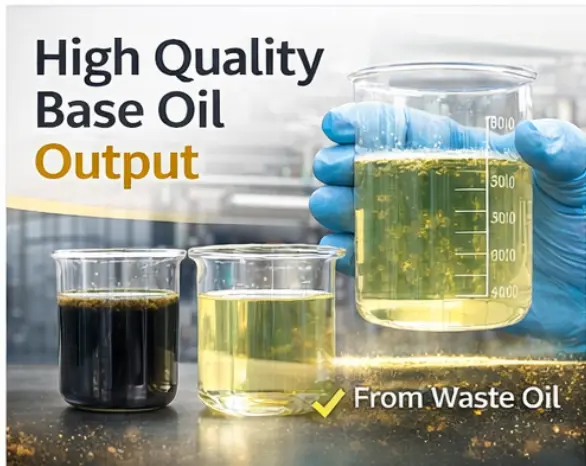
VBOLT base oil solvent extraction unit is a dedicated deep refining system for base oil production from waste lube oil regeneration. Equipped with advanced solvent extraction and refining processes, it effectively removes sulfur, nitrogen, aromatic hydrocarbons, colloids and various impurities from regenerated base oil, and finally produces premium Group I & Group II base oil in full compliance with API standards.
System Scope
Extraction Unit · Separation Unit · Solvent Recovery · Product Tanking
Product Overview
The VBOLT Base Oil Solvent Extraction Plant is a professional deep refining system for waste lubricant re-refining and regenerated base oil upgrading, which adopts high-efficiency selective solvent extraction technology to effectively remove sulfur, nitrogen, aromatics, colloids and oxidized impurities from recycled crude base oil and steadily produce high-quality Group I & Group II(close to) base oils that meet API standards; featuring low energy consumption, full automation, and customizable capacity, our turnkey solution is ideal for waste oil recycling and high-grade regenerated base oil production.
———— Our Working Process
How VBOLT Base Oil Solvent Extraction Works
VBOLT uses selective solvent extraction, vacuum solvent recovery, steam stripping, and drying to remove undesirable components from recycled base oil and improve refining performance.
This process is widely used in waste lubricant oil regeneration, used oil re-refining and high-quality recycled base oil production projects.
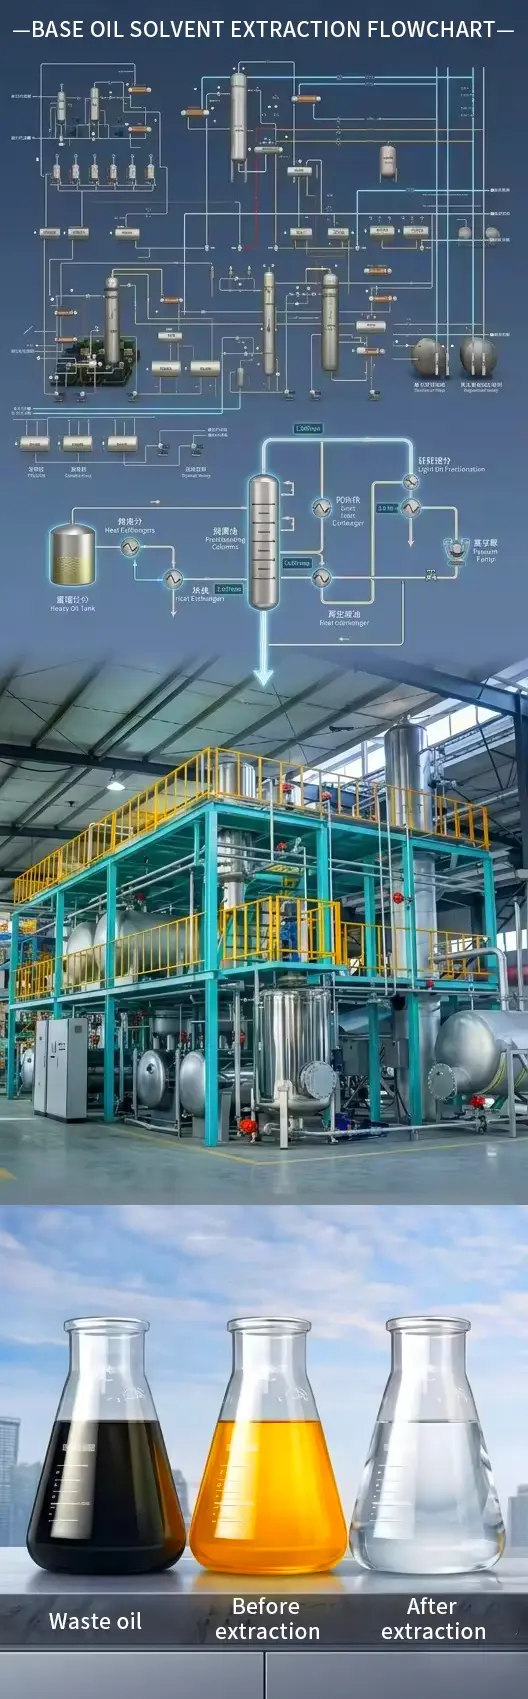
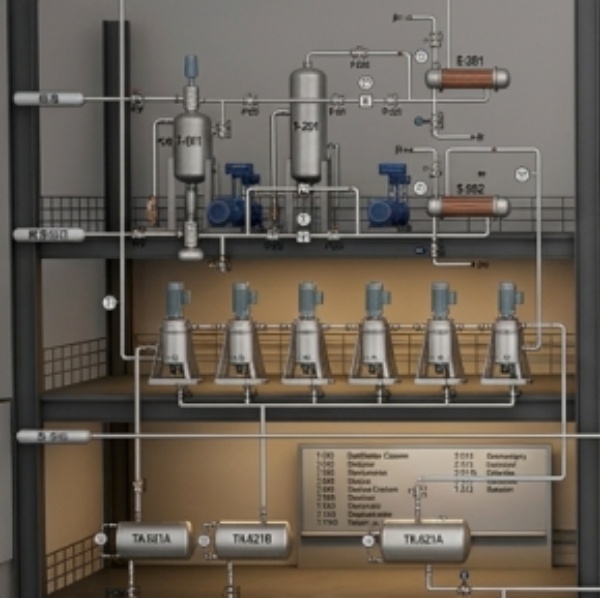
Base Oil Solvent Extraction Integrated Process Flow Scheme
VBOLT Base Oil Solvent Extraction Plant is designed to refine regenerated oil by removing sulfur, nitrogen, aromatics, and other contaminants, helping produce high-quality base oil for industrial applications.
The base oil and NMP solvent are separately heated by heat exchange to about 60°C, creating suitable temperature conditions for the subsequent countercurrent extraction. This helps maintain a stable density difference between the two phases and lays the foundation for efficient mass transfer.
The base oil enters from the lower part of the centrifugal extractor, while the NMP solvent enters from the upper part. Countercurrent extraction is carried out at a solvent-to-oil ratio of about 0.85:1. By utilizing the density difference between the two phases, saturated hydrocarbons (refined base oil components) are efficiently separated from undesirable components such as resins and asphaltenes.
The refined base oil obtained from extraction is sent to the refined oil recovery tower. After heat exchange, it is heated to 170°C and subjected to flash evaporation under a vacuum of -85 kPa, removing 99.8% of the residual NMP solvent. The recovered solvent is condensed and returned to the solvent tank for recycling.
The refined oil from the recovery tower is then sent to a stripping tower, where it comes into countercurrent contact with superheated steam at 0.5 MPa and 200°C. This removes trace amounts of dissolved NMP from the oil, reducing solvent residue to an extremely low level while further improving product quality.
After stripping, the refined oil is heated to 140°C through heat exchange and sent to a drying tower, where trace moisture is removed under vacuum conditions. The water vapor is condensed and then treated through oil-water separation, ensuring that the moisture content of the base oil meets specification requirements.
The extract phase obtained from extraction is sent to the extract recovery tower. It first exchanges heat with the NMP solvent vapor generated inside the tower, and is then heated to 165°C by thermal oil. Under a vacuum of -65 kPa, 99.98% of the NMP solvent is evaporated and recovered. The recovered solvent is condensed and recycled.
After solvent recovery, the bottom product of the recovery tower contains undesirable components such as resins and asphaltenes, which are separated as bottom oil. This ensures complete separation of impurities from the effective solvent and prevents solvent contamination.
The NMP solvent recovered from each process section is collected in the solvent tank for cyclic reuse. A small amount of uncondensed light components and NMP-containing non-condensable gases are treated in a water-seal tank, and then sent to the heating furnace as fuel, achieving harmless off-gas treatment and energy recovery.
Core Engineering Advantages
The system is purpose-built for practical industrial base oil refining operations, with a strong focus on oil recovery efficiency, ultra-high solvent recycling rate, stable process control, and flexible project implementation.
Solvent Recovery Efficiency
Complete solution from raw base oil preheating, centrifugal counter-current extraction, solvent recovery, steam stripping, drying to final product storage.
Full industrial-duty configuration, engineered for non-stop production runs with minimal downtime and robust process stability.
Modular integration suitability for export and fast installation
Main Equipment Configuration
Equipment selection depends on processing capacity, feed composition, solvent system, utility conditions and automation scope. A standard configuration usually includes the following units.
Main Process Equipment
Used Oil Storage Tank
Feed Pump and Transfer Piping
Feed Heater / Heat Exchanger
Filtration Unit / Pretreatment Device
Solvent Dosing Tank and Pump
Extraction Tank / Reactor / Mixer
Settling Tank / Separation Vessel
Base Oil Product Tank
Residue / Sludge Tank
Recovery & Auxiliary Equipment
Solvent Recovery Column or Evaporation Unit
Condenser and Recovery Tank
Solvent Circulation Tank
Vacuum System (Optional)
Product Polishing Filter (Optional)
Control Valves and Instrumentation
Explosion-proof Electrical Components
Vent Condensation / Safety System
Skid Frame / Modular Integration Structure
Applicable Feedstocks
This type of equipment is widely applicable to waste lubricating oil recycling and similar oil recovery projects where base oil recovery and impurity reduction are important.
Why Customers Choose This Solution
This equipment route is attractive for industrial clients looking for a practical, scalable, and commercially viable used oil regeneration process.
Delivers odor-free finished products with improved purity and performance, meeting the quality requirements of Group I and Group II base oils.
The solvent can be recycled multiple times, with total solvent consumption kept below 0.5%, significantly lowering operating expenses.
The process generates no solid waste, making it especially suitable for regions with strict environmental compliance standards.
Effectively replaces silica gel and clay-based treatments, which are associated with higher costs and substantial waste generation.
Automated process control minimizes manual intervention, reducing labor costs while lowering the risk of operational errors.
Designed for continuous operation with low maintenance requirements, ensuring stable performance and productivity in 24/7 industrial applications.
Frequently Asked Questions
Common inquiries from buyers interested in base oil recovery and solvent extraction equipment.
Get a Base Oil Extraction Proposal
Send us your feedstock information, required capacity, product target and project location. We can prepare a technical proposal, equipment configuration suggestion and modular solution recommendation.